GN Separation has developed a customized decanter centrifuge for a canola oil clarification project in Australia. Specifically designed for edible oil processing, this solution focuses on efficient solid-liquid separation while addressing key requirements for hygienic operation, process flexibility, and long-term reliability.
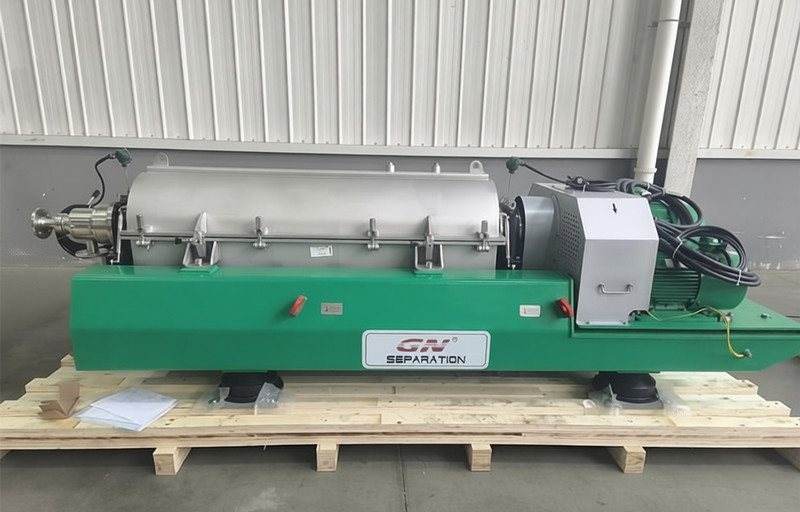
For this project, GN paid particular attention to the centrifuge's internal design to meet the specific requirements of edible oil applications. One key feature is the polished finish applied to the internal screw conveyor. The screw surface is carefully polished to reduce material adhesion and minimize the accumulation of residual material inside the machine. This is especially important in food processing, where material buildup may deteriorate over time and potentially affect product hygiene. The smoother surface also facilitates internal cleaning and helps maintain a cleaner operating environment.
Another important feature is the use of a centripetal pump for clarified liquid discharge. Compared with conventional discharge arrangements that may require the centrifuge to be stopped for adjustment, this design allows operators to adjust the liquid pool depth while the machine is running. By changing the pool depth, operators can optimize separation conditions to suit variations in feed characteristics and production requirements. This flexibility helps reduce unnecessary downtime and supports more continuous, efficient operation.
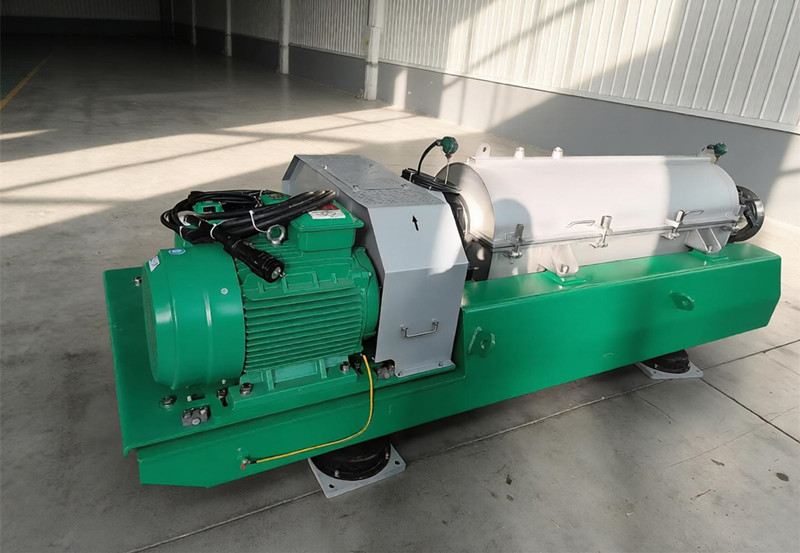
Beyond these customized features, the decanter centrifuge is designed for stable, continuous operation and reliable separation performance. Its compact structure, continuous solids discharge, and adjustable operating parameters make it suitable for integration into industrial edible oil processing lines. The equipment configuration is tailored to the customer's process requirements, aiming to balance separation efficiency, product quality, and ease of operation.
GN Separation has extensive experience in designing and manufacturing industrial decanter centrifuges for a wide range of applications, including food processing, wastewater treatment, oil and gas, and mining. Since materials and operating conditions vary from project to project, GN focuses on adapting its separation technology and equipment configurations to meet specific application requirements.
This canola oil clarification project in Australia reflects GN's commitment to application-specific equipment design. By combining a polished internal screw conveyor with flexible liquid pool depth adjustment, GN aims to provide a reliable separation solution that supports efficient processing and consistent product quality.